In the constantly changing world of industrial applications, picking the right components really makes a difference when it comes to keeping things running smoothly and reliably. One component that's been getting a lot of attention lately is the Api 608 Ball Valve. If you ask industry folks, like James Anderson from Fluid Control Solutions, he’ll tell you, “The API 608 Ball Valve isn’t just any valve — it’s a symbol of quality and performance that can really boost safety and efficiency on the job.”
Thanks to its sturdy design and ability to handle different pressures and temperatures, the API 608 Ball Valve has become a go-to for engineers and operators alike. Its features, like a tight seal and low torque requirements, make it perfect for managing critical processes in industries like oil and gas, chemical processing, and water treatment.
In this article, we’ll dive into the top five benefits of using API 608 Ball Valves in industrial settings. We’ll see how their standout features help improve, well, operational performance and reliability, even in some pretty tough environments.
Overview of API 608 Ball Valves in Industrial Settings
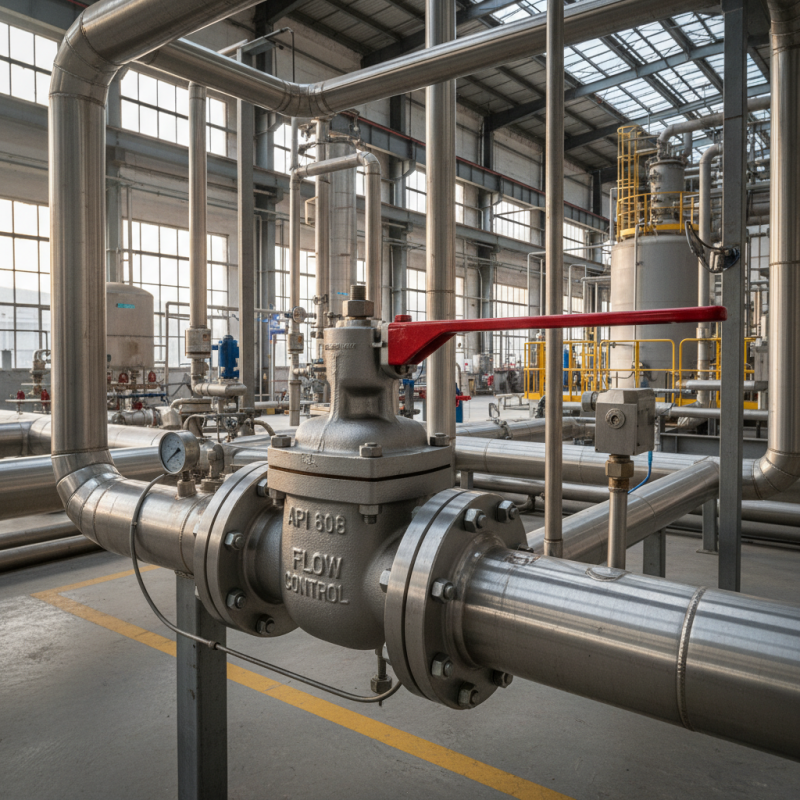
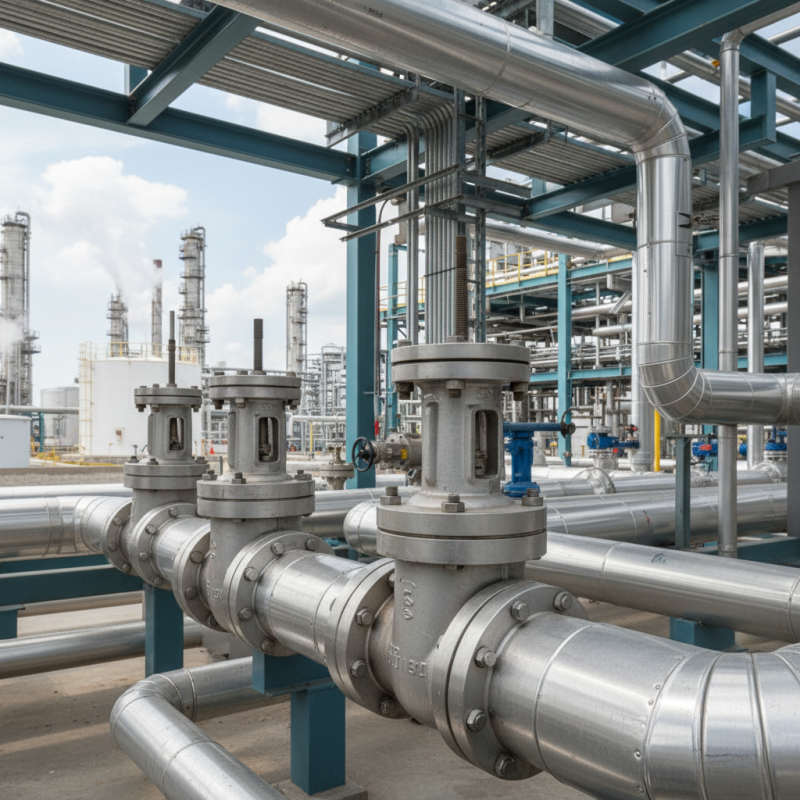
API 608 ball valves play a crucial role in industrial applications, thanks to their robust design and reliable performance. These valves, manufactured in compliance with the American Petroleum Institute's standards, are specifically engineered for use in high-pressure and high-temperature conditions, making them ideal for various processes in sectors such as oil and gas, chemical processing, and water treatment. The construction materials often used, like stainless steel or carbon steel, provide excellent corrosion resistance and durability, ensuring the valves can handle harsh environments without compromising functionality.
In addition to their durability, API 608 ball valves offer exceptional ease of operation. Their quarter-turn design allows for quick open or close actions, facilitating efficient fluid control. This feature is particularly beneficial in industrial settings where swift response times are necessary to maintain safety and productivity. Additionally, the tight sealing capability of these valves minimizes the risk of leaks, contributing to overall system integrity and reliability. As industries continue to prioritize safety and efficiency, the adoption of API 608 ball valves will only increase, reinforcing their significance in modern industrial operations.
Key Features of API 608 Ball Valves
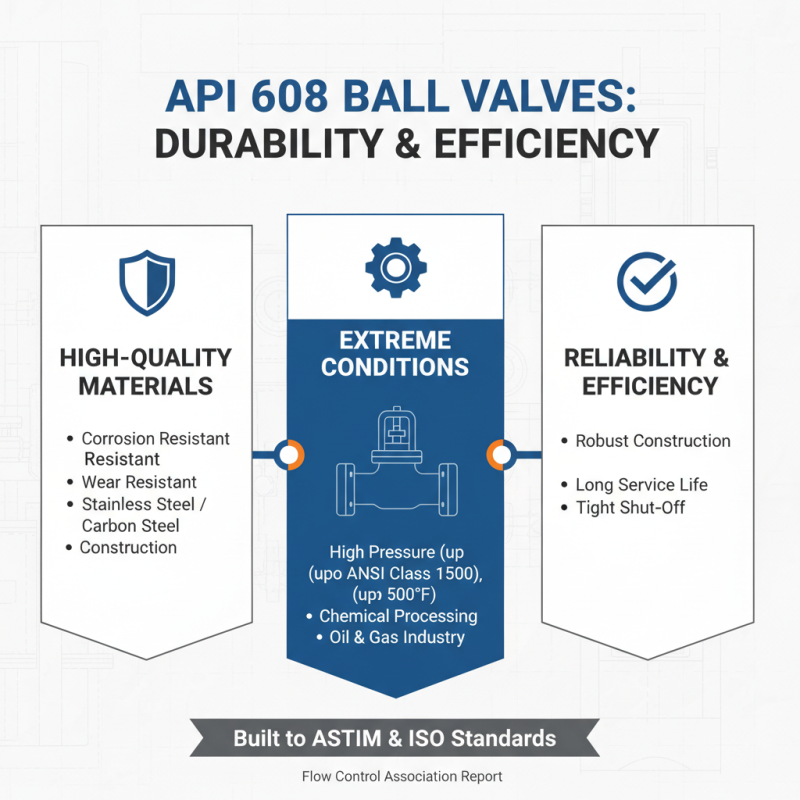
API 608 ball valves are widely recognized in industrial applications for their durability and efficiency, thanks to several key features. Firstly, they are constructed with high-quality materials that provide excellent resistance to corrosion and wear. According to a report by the Flow Control Association, these valves can withstand high pressures and temperatures, making them ideal for demanding environments, such as chemical processing and oil and gas industries. The ability of API 608 valves to maintain structural integrity under extreme conditions highlights their reliability.
Another significant feature of API 608 ball valves is their full port design, which ensures minimal pressure drop across the valve and improves flow efficiency. This design characteristic is particularly beneficial in applications where maintaining flow rates is crucial. A study published by the Valve Manufacturers Association states that using full-port ball valves can optimize system performance by reducing energy consumption and enhancing system reliability. Additionally, API 608 valves offer a tight sealing mechanism, preventing leaks and promoting safety in fluid handling processes.
Enhanced Flow Control with API 608 Ball Valves
API 608 ball valves are increasingly recognized for their ability to enhance flow control in a variety of industrial applications. These valves, known for their robust construction and reliability, provide superior leakage protection and quick shut-off capabilities. According to a report by Grand View Research, the global ball valve market is projected to reach USD 12.3 billion by 2025, driven by the increasing demand for reliable flow control solutions across industries such as oil and gas, water treatment, and chemical manufacturing.
WELCO Valve Co., Ltd. specializes in the research, design, and production of a wide range of valves, including API 608 ball valves. Our commitment to quality and innovation enables us to meet the diverse needs of our clients with precision-engineered products. The API 608 standard ensures that these ball valves are suitable for high-pressure applications, with the ability to maintain flow rates efficiently while minimizing turbulence and resistance. As industries seek to improve operational efficiency, the adoption of API 608 ball valves becomes crucial in achieving enhanced flow control, which is vital for maintaining system integrity and reducing downtime.
Durability and Longevity of API 608 Ball Valves
API 608 ball valves are renowned for their durability and longevity, making them an excellent choice for industrial applications. Manufactured from high-quality materials, these valves can withstand harsh operating conditions, including extreme temperatures and pressures. The robust design not only enhances their performance but also minimizes the risk of leaks and failures, which is critical in industrial environments where safety and efficiency are paramount.
Furthermore, the longevity of API 608 ball valves can significantly reduce maintenance costs and downtime. Their ability to resist corrosion and wear ensures that they maintain their operational integrity over time, resulting in fewer replacements and repairs. This durability is particularly advantageous in industries such as oil and gas, petrochemical, and water treatment, where reliability and continuous operation are essential for productivity and profitability. By investing in API 608 ball valves, organizations can enhance their operational efficiency while ensuring long-term performance and safety.
Top 5 Benefits of Using API 608 Ball Valves in Industrial Applications
Cost-Effectiveness of Using API 608 Ball Valves
In industrial applications, the cost-effectiveness of using API 608 ball valves is particularly noteworthy. According to a report by Market Research Future, the global valve market is projected to grow significantly, driven by factors like automation and efficiency. API 608 ball valves, known for their durability and reliability, play a crucial role in maintaining operational efficiency while minimizing costs. Their reduced pressure drop compared to traditional valves enhances energy savings, ultimately leading to lower operational expenses.
Additionally, API 608 ball valves are designed for longevity, which further contributes to their cost-effectiveness. A study from the Industrial Valves Association indicates that the long service life of these valves can reduce maintenance and replacement costs by up to 25%. This durability not only decreases downtime but also significantly cuts repair costs, positioning API 608 ball valves as a financially savvy choice for industries where budget constraints are prevalent. Ultimately, investing in these valves can lead to substantial savings without compromising performance, making them an attractive option for industrial applications.
Applications of API 608 Ball Valves in Various Industries
API 608 ball valves are widely utilized across various industries due to their robust construction and reliable performance. The oil and gas sector, in particular, benefits significantly from these valves, as they are designed to handle high-pressure applications and extreme temperatures. According to a recent report by Transparency Market Research, the global ball valve market is projected to reach $8 billion by 2026, with a significant portion attributed to API 608 compliant valves, which ensure safety and efficiency in flow control. These valves offer excellent sealing capabilities, minimizing leakage and enhancing operational reliability in critical scenarios.
In the chemical processing industry, the versatility of API 608 ball valves enables seamless integration into various systems, facilitating the efficient handling of corrosive fluids and gases. A study published by Grand View Research highlights that the chemical processing sector accounts for approximately 30% of the total ball valve market share, with an increasing demand for API-compliant products. The ability of these valves to provide tight shut-off and reducing maintenance requirements is paramount in improving productivity and ensuring compliance with industry safety standards.
Top 5 Benefits of Using API 608 Ball Valves in Industrial Applications
| Benefit | Description | Applications |
| Durability | Designed to withstand harsh conditions, reducing the need for frequent replacements. | Oil and gas, chemical processing |
| High Flow Rate | Offers minimal resistance to flow, enhancing efficiency. | Water treatment, HVAC systems |
| Versatility | Suitable for various media including liquids, gases, and slurries. | Food & beverage, pharmaceuticals |
| Ease of Operation | Can be operated manually or automatically with simple mechanisms. | Power generation, pulp & paper |
| Sealing Capability | Provides effective sealing with low leakage rates, ensuring safety. | Mining, petrochemical |
Comparison with Other Valve Types in Industrial Use
When comparing API 608 ball valvesto other valve types in industrial applications, several distinct advantages become clear. API 608 ball valves are renowned for their reliable sealing capabilities, which outperform gate and globe valves, particularly in high-pressure environments. Unlike Gate Valves that may experience wear over time due to frequent operation, ball valves offer minimal resistance and ensure atight seal even after extended use. This efficiency results in reduced leakage and greater safety in critical industrial processes.
Additionally, the ease of operation of API 608 ball valves sets them apart. While other types, such as butterfly or check valves, may require more complex control mechanisms, ball valves provide straightforward open and close functionality with a simple quarter-turn. This design not only facilitates faster installation and maintenance but also enhances overall operational efficiency. Moreover, their durable construction makes them suitable for a wide range of temperatures and pressures, unlike some valve types that have more limited operating conditions. These characteristics make API 608 ball valves a preferred choice for industries prioritizing reliability and performance.
Comprehensive Guide to the BS 1873 Bolted Bonnet Globe Valve: Features, Benefits, and Applications
The BS 1873 Bolted Bonnet Globe Valve is a robust and versatile choice for various industrial applications, particularly known for its reliability and efficiency in controlling fluid flow. With a nominal diameter of 6 inches and a pressure rating of ANSI Class 150#, this valve is engineered to withstand substantial operational demands. Its construction using ASTM A216 WCB material ensures not only durability but also corrosion resistance, making it suitable for a wide range of environments.
One of the key features of this valve is its bolted bonnet design, which facilitates easy maintenance and provides a reliable seal to prevent leaks. The valve operates via a handwheel, allowing for smooth and precise control over the flow rate. Additionally, the rising stem and outside screw and yoke (OS&Y) configuration enhance accessibility for monitoring and maintenance tasks. The plug disc design optimizes flow characteristics and minimizes pressure drops, making it an effective solution for applications requiring tight shut-off and efficient flow regulation. The RF flanged connection, adhering to ASME B16.5 standards, further simplifies installation and integration into existing systems.
FAQS
PI 608 ball valves primarily used for in industrial settings?
API 608 ball valves are often constructed from materials like stainless steel or carbon steel, which provide excellent corrosion resistance and durability.
API 608 ball valves feature a quarter-turn design that allows for quick open or close actions, making them easy to operate and facilitating efficient fluid control.
The tight sealing capability of API 608 ball valves minimizes the risk of leaks, contributing to overall system integrity and reliability, which are crucial for maintaining safety and productivity in industrial operations.
API 608 ball valves provide superior leakage protection and quick shut-off capabilities, making them highly effective for enhancing flow control while maintaining efficient flow rates.
The demand for API 608 ball valves is particularly growing in the oil and gas sector, water treatment, and chemical manufacturing industries.
The global ball valve market is projected to reach USD 12.3 billion by 2025, with significant growth attributed to the increasing demand for API 608 compliant valves.
In the chemical processing industry, API 608 ball valves facilitate the efficient handling of corrosive fluids and gases while providing tight shut-off and reducing maintenance requirements.
WELCO Valve Co., Ltd. specializes in the research, design, and production of a wide range of valves, including API 608 ball valves, ensuring precision-engineered products that meet diverse client needs.
The chemical processing sector accounts for approximately 30% of the total ball valve market share, highlighting the increasing demand for API-compliant products in this industry.
Conclusion
API 608 Ball Valves are essential components in various industrial applications, offering numerous advantages that enhance operational efficiency. These valves are designed to provide exceptional flow control, making them ideal for managing the movement of fluids in a wide range of settings. Their key features include robust durability and longevity, ensuring they withstand the rigors of industrial environments. Additionally, API 608 Ball Valves are cost-effective, providing long-term savings through reduced maintenance and replacement costs.
WELCO Valve Co., Ltd. recognizes the significance of API 608 Ball Valves, as their versatile applications span multiple industries, including oil and gas, water treatment, and chemical processing. When compared to other valve types, API 608 Ball Valves excel in performance, reliability, and efficiency, solidifying their position as a preferred choice for industrial operations. With a commitment to quality and innovation, WELCO Valve Co., Ltd. continues to support the diverse needs of industries through their extensive range of valve solutions.