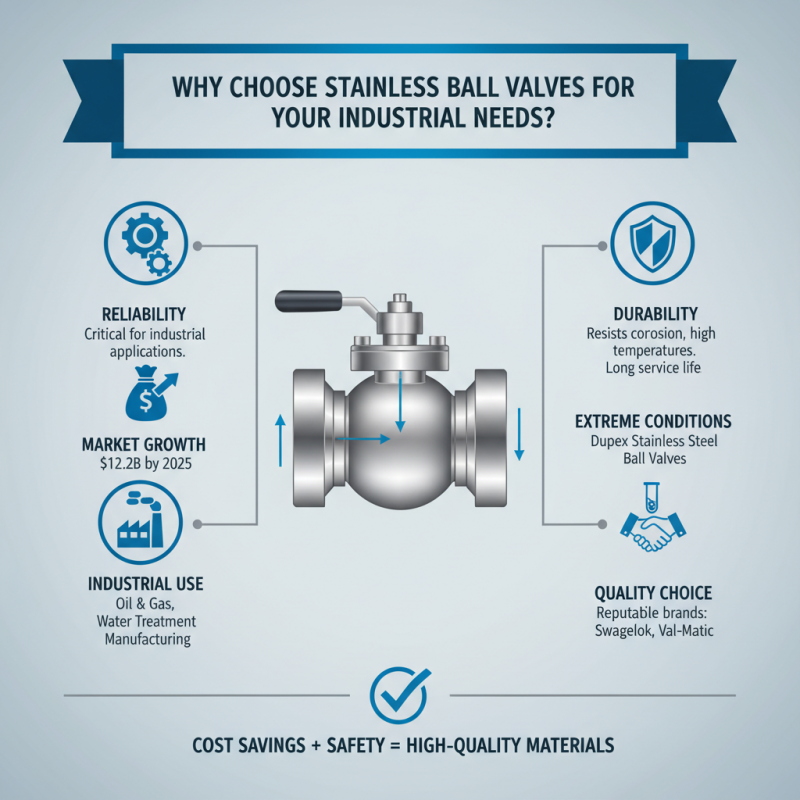
When it comes to industrial applications, reliability isn't just important – it's everything. One key component that really helps boost reliability is the stainless steel ball valve. I read somewhere that the global market for ball valves is projected to hit around $12.2 billion by 2025, mainly because industries are really craving efficient flow control options right now. Stainless Ball Valves are pretty much a must-have in sectors like oil and gas, water treatment, and manufacturing thanks to their toughness.
What’s great about stainless ball valves is that they resist corrosion and can handle high temperatures without breaking a sweat. That durability means they last a long time, which means fewer replacements and less hassle. For example, check out a Duplex Stainless Steel Ball Valve — it’s built to handle some really extreme conditions, making it a favorite in tough environments. But, honestly, not all stainless ball valves are created equally. Some might not meet the strict standards industries require, which could lead to failures or problems down the line.
Picking the right valve isn’t just about size or price — you’ve gotta consider quality too. Not every manufacturer is the same, so it’s smart to stick with trusted names like Swagelok or Val-Matic. It might cost a bit more upfront, sure, but the savings on maintenance and avoiding downtime really add up in the long run. Still, never underestimate the importance of choosing high-quality materials — that’s the foundation for reliable performance in any industrial setup.
Advantages of Stainless Ball Valves in Industrial Applications
Stainless ball valves are a popular choice in many industrial applications. Their robust construction makes them suitable for various environments. These valves can handle high pressure and temperature, providing reliability. In industries such as oil and gas, water treatment, and food processing, durability is a must. Stainless Steel Ball Valves resist corrosion, ensuring a long lifespan. This resistance also leads to lower maintenance costs over time.
Moreover, the smooth operation of stainless steel ball valves allows for easy control of fluid flow. They provide quick shut-off capabilities, essential in emergency situations. The design of these valves minimizes leakage risks, which adds to their appeal. However, installing the correct size and type is crucial. Improper installation can lead to issues, impacting the entire system’s efficiency. It’s vital to assess specific needs and conditions.
Even with many advantages, challenges exist. Selecting the right material grade for the stainless steel ball valve is critical. Not every application will suit all grades. Understanding the environment and potential chemical exposure can prevent costly errors. Despite these challenges, the benefits often outweigh the downsides. In many cases, they remain the go-to solution for industrial needs.
Comparison with Other Valve Types: Why Stainless Stands Out
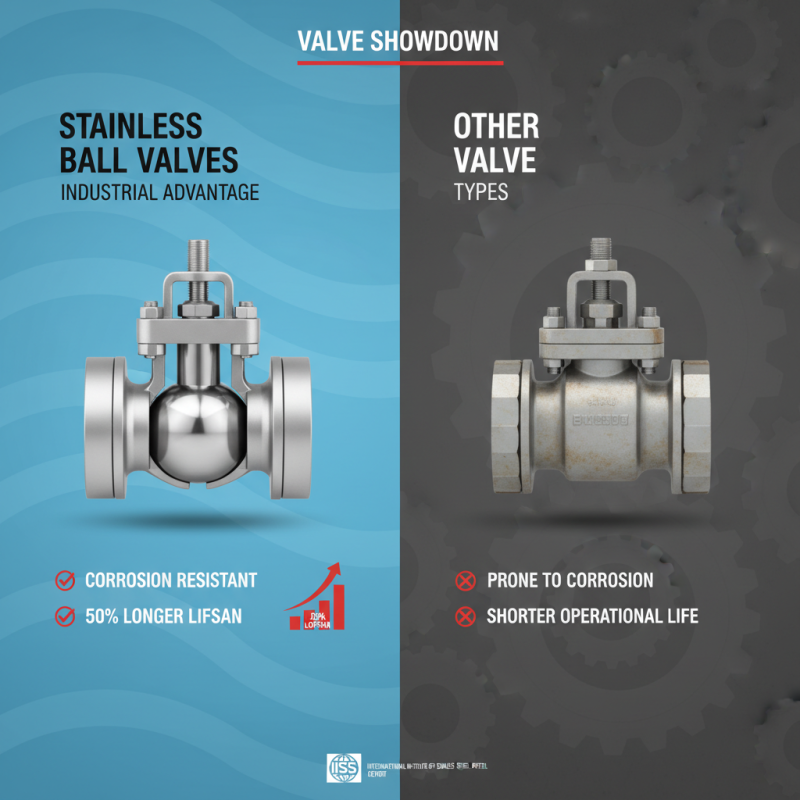
When comparing valve types for industrial applications, Stainless Ball Valves often come out on top. Their corrosion resistance is unmatched. According to a recent report by the International Institute of Stainless Steel, these valves can outperform others in harsh environments. For instance, they show a significant longevity increase, lasting up to 50% longer than other valve options.
Stainless ball valves also offer superior flow control. A study by the Valve Manufacturers Association highlights that these valves maintain a tighter seal. This capability minimizes leakage, a critical factor in industries like oil and gas. Compared to gate or Globe Valves, stainless ball valves can reduce energy costs by optimizing flow rates. Yet, some users may face installation challenges. The maintenance required can be somewhat demanding, particularly in older systems.
However, the cost-effectiveness of stainless ball valves should not be overlooked. They may come with a higher upfront cost. Still, lower maintenance needs and improved efficiency often lead to greater savings over time. This balance of initial investment and long-term benefits complicates the decision. Users must weigh the short-term expenses against eventual gains, a reflective process necessary for making informed choices.
Durability and Corrosion Resistance of Stainless Ball Valves
Stainless ball valves are increasingly favored in industrial applications. Their durability and corrosion resistance are unparalleled. In environments with corrosive substances, these valves excel. A recent industry report indicates that stainless steel can resist oxidation and corrosion better than many other materials. This makes stainless ball valves ideal for chemical processing, oil and gas, and water treatment sectors.
The lifecycle of stainless ball valves is impressive. Many can last over 25 years under normal conditions. This longevity reduces the need for replacements. According to studies, facilities using stainless steel components see a 15% decrease in maintenance costs. Moreover, the smooth operation of ball valves prevents leaks, enhancing system efficiency. Such reliability builds a strong case for choosing stainless ball valves.
However, not all are aware of the different grades of stainless steel. Choosing the wrong grade can lead to premature failure. This decision often reflects a lack of knowledge about material properties. Stainless Steel Ball Valve China offers various options, but understanding their features is crucial. Investing time in this research can pay off in the long run.
Design and Functionality: How Stainless Ball Valves Operate
Stainless ball valves are crucial in many industries. Their design promotes efficient flow control. These valves consist of a hollow, perforated sphere. When the valve is turned, the flow is either blocked or allowed through. This simple mechanism is reliable and effective.
The functionality of stainless ball valves offers advantages that are hard to ignore. They provide tight sealing, which minimizes leaks. This is vital in settings where pressure and safety are concerns. The smooth surface of the stainless steel, including options like China Duplex Stainless Steel Ball Valve, reduces corrosion. This prolongs the valve's lifespan, making it a cost-effective choice.
In industrial applications, these valves can handle high temperatures. However, not all environments are perfect. Sometimes, buildup can affect performance. Regular maintenance is essential to ensure they operate as intended. Users must be aware of their surroundings and act accordingly. Proper use enhances reliability and prevents failures.
Cost-Effectiveness: Long-Term Benefits of Choosing Stainless
Stainless ball valves are a popular choice for many industrial applications. Their durability is a key factor. Unlike other materials, stainless steel resists corrosion and extreme temperatures. This means fewer replacements over time.
Cost-effectiveness is another reason to choose stainless. While the initial investment might be higher, long-term savings kick in quickly. Maintenance costs drop significantly due to the valve's sturdy construction. Many industries overlook this important detail. Ignoring durability can lead to expensive downtimes.
Additionally, stainless steel offers reliable performance across various environments. Even with harsh chemicals, these valves hold up well. This reliability saves money in the long run. However, some users find maintenance can be tricky. A thorough understanding is necessary. Regular checks are vital to ensure optimal operation. Keeping track of performance can be daunting but rewarding.
Why Choose Stainless Ball Valves for Your Industrial Needs? - Cost-Effectiveness: Long-Term Benefits of Choosing Stainless
| Feature | Stainless Ball Valve | Other Valve Types |
| Corrosion Resistance | Excellent | Moderate to Low |
| Durability | High | Variable |
| Maintenance Frequency | Low | High |
| Initial Cost | Moderate | Low |
| Life Span | 25+ years | 10-15 years |
| Efficiency | High | Variable |
| Suitability for High Pressure | Yes | Depends on Type |
Maintenance Considerations for Stainless Ball Valves
Maintaining stainless ball valves requires attention to several critical aspects. Proper upkeep significantly extends their lifespan, which can average 15 to 20 years in industrial settings. Regular inspections are vital. A key focus should be on leakage points, as reports indicate that up to 30% of valve failures are due to wear and tear in seals.
Lubrication is another essential maintenance step. Many operators overlook this, undermining performance. A study shows that 20% of valve malfunctions are linked to inadequate lubrication. Moreover, operators should periodically check for corrosion, especially in harsh environments. Though stainless steel is resistant, it’s not immune to pitting or stress corrosion.
Cleaning is often forgotten yet crucial. Deposits can affect valve operation. It might be necessary to install strainers to minimize debris ingress. Choosing the right cleaning agents matters; harsh chemicals can cause more harm than good. It’s important to strike a balance between effectiveness and material safety. This requires a well-thought-out maintenance plan determined by facility needs. Remember, proactive care is always more effective than reactive measures.
Applications of Stainless Ball Valves in Various Industries
Stainless ball valves are essential in many industries. They are durable and resistant to corrosion. This makes them ideal for applications in chemical processing. These valves handle harsh substances safely. Their design allows for quick and precise control of flow rates. This is crucial in manufacturing settings to maintain efficiency.
In the food and beverage industry, stainless ball valves ensure hygiene. They are easy to clean and maintain. This prevents contamination during production. The pharmaceutical sector benefits as well. Precise control is necessary when dealing with sensitive compounds. Yet, the choice of ball valves must consider compatibility with various fluids.
Challenges exist when selecting these valves. Not all stainless steel grades suit every application. Certain environments can lead to wear or mechanical failure. It’s vital to assess your specific needs. Without careful consideration, long-term reliability may suffer. Proper installation and regular maintenance can mitigate some of these risks.
FAQS
: The service aims to provide assistance and information. It helps users find solutions to various issues.
You can access it through the website or mobile app. Just follow the prompts to get started.
Generally, the basic features are free. Some premium options may involve a fee. Check the details.
It addresses common questions, technical problems, and offers guidance on many topics.
Response times vary. Some inquiries are answered promptly, while others may take longer to resolve.
Yes, support is available 24/7. However, immediate help may not always be guaranteed.
You can resubmit your inquiry or ask for escalation. Persistence helps in finding the right solution.
Yes, certain complex issues might require in-depth assistance. Not all problems can be solved quickly.
Yes, users can request updates. It’s okay to check back if you feel anxious about unresolved issues.
User data is treated confidentially, though there are always risks online. Reflect on privacy while using services.
Conclusion
Stainless ball valves are increasingly favored in industrial applications due to their remarkable advantages, which include durability, corrosion resistance, and economic viability. Unlike other valve types, stainless ball valves exhibit superior longevity and performance in harsh environments, ensuring a reliable solution for various industrial needs. Their design facilitates smooth operation and efficient flow control, making them essential in multiple sectors.
Furthermore, the long-term cost-effectiveness of stainless ball valves is significant, as their robust construction requires less frequent maintenance and replacement. Industries ranging from chemical processing to water treatment leverage the benefits of stainless ball valves, reinforcing their role as a standard choice for modern industrial applications. Overall, the combination of durability, efficiency, and low maintenance makes the stainless ball valve a standout option for any industrial setting.