When it comes to industrial setups, having piping systems that are both efficient and reliable is absolutely crucial. And one key component that really helps keep these systems running smoothly is the Floating Ball Valve. I came across a report from Research and Markets that said the global ball valve market was worth around $2.5 billion back in 2020. And guess what? They’re expecting it to grow at a steady rate of about 4.5% each year over the next few years. This just shows how much industries like oil and gas, water treatment, and chemicals need dependable valve solutions that perform consistently.
Floating ball valves are pretty popular because they’re simple to use and don’t overcomplicate things. One of their biggest perks is the floating mechanism — it lets the ball move just a tiny bit within the seat, which makes for a tighter seal. That means less chance of leaks, even when pressures fluctuate. I also saw a report from Allied Market Research noting that as industries push more into automation and smarter control systems, the demand for high-performance valves is skyrocketing. And among all options out there, floating ball valves are really catching the eye of engineers and procurement folks alike.
As technology keeps advancing and regulations get tougher, picking the right valve isn’t just a small detail — it’s a big deal. Getting to understand how floating ball valves work and where they fit in can actually give your business a leg up. They help keep operations running smoothly and boost safety, which is pretty much what everyone’s looking for in a good piping system.
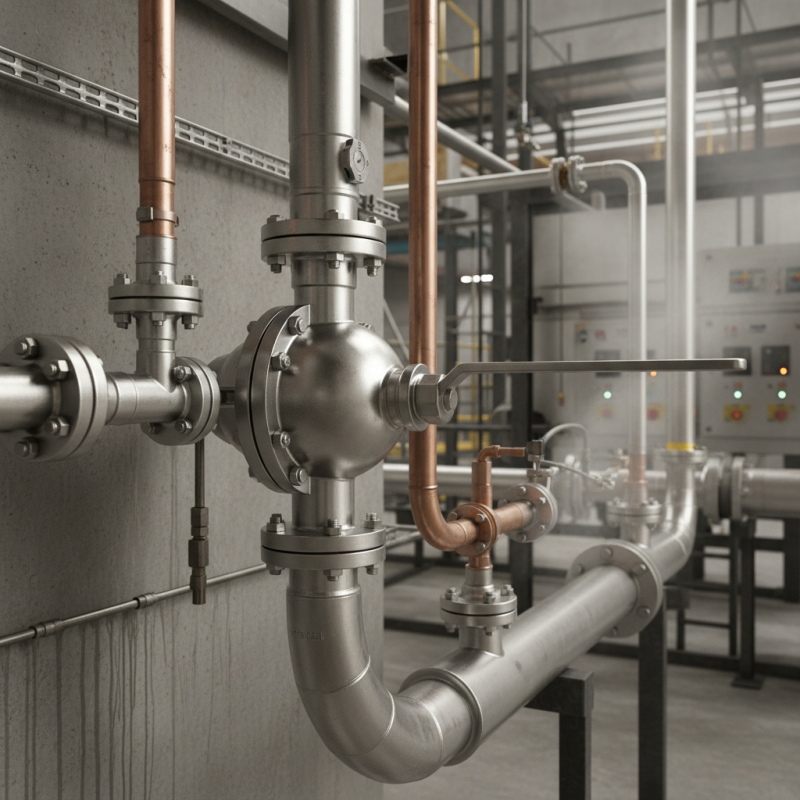
Floating ball valves have become a popular choice in industrial applications due to their inherent advantages in reliability and efficiency. One of the key benefits of floating ball valves lies in their design, which allows the ball to float within the seat. This means that any pressure applied to the upstream side is transmitted directly to the ball, ensuring a tight seal. According to the Valve Manufacturers Association, floating ball valves can achieve a leakage rate as low as 0.01% of the inlet flow rate, making them ideal for critical applications where minimizing leaks is paramount.
Furthermore, floating ball valves offer ease of operation and maintenance. They allow for quick isolation of flow, which is crucial during maintenance or emergency situations. Data from the American National Standards Institute indicates that using floating ball valves can reduce downtime by up to 25% compared to other valve types, leading to significant cost savings over time. Their simplicity in design also means fewer components that could fail, ensuring improved system reliability and extended service life.
Tips: When selecting floating ball valves for your system, consider factors such as fluid characteristics, pressure rating, and temperature range to ensure optimal performance. Regularly inspecting and maintaining the valves can prevent undue wear and tear, thus ensuring their longevity. Additionally, investing in high-quality materials for critical applications can further enhance performance and safety in industrial environments.
| Advantage | Description | Application Area | Material Compatibility |
|---|---|---|---|
| Durability | Floating ball valves are designed to withstand high pressures and temperatures, ensuring a long service life. | Chemical Processing, Oil & Gas | Stainless Steel, Brass, PVC |
| Easy Operation | These valves operate with a simple quarter-turn mechanism, allowing for quick shut-off. | Water Treatment, HVAC | CPVC, POM |
| Compact Design | Floating ball valves have a smaller footprint, making them ideal for tight spaces in piping systems. | Food & Beverage, Pharmaceuticals | Hastelloy, PTFE |
| Leak Prevention | Designed to provide a tight seal with minimal risk of leaks, contributing to system integrity and safety. | Mining, Waste Management | Titanium, Carbon Steel |
| Versatility | Can be used in various applications and media types, from gases to liquids, making them highly adaptable. | Energy, Construction | Various alloys, Plastic materials |
Floating ball valves are essential components in industrial piping systems, offering distinct advantages over other valve types. One of the key features of floating ball valves is their design, which allows the ball to move slightly within the valve body. This self-adjusting ability ensures a tight seal when closed, effectively preventing leaks. Unlike other valve types, such as gate or Globe Valves, floating ball valves operate with minimal pressure drop, making them ideal for high-flow applications where efficiency is critical.
Additionally, floating ball valves are renowned for their ease of operation and maintenance. The simple quarter-turn mechanism enables quick opening and closing, making them user-friendly. In contrast, other valve types may require more complex actuation methods or are subject to more wear and tear due to their intricate designs. The robust construction of floating ball valves also ensures durability and reliability, even in demanding environments, which is crucial for minimizing downtime and maintenance costs in industrial settings.
Furthermore, floating ball valves can accommodate a wide range of temperatures and pressures, making them versatile across various applications. This adaptability is not always found in other types of valves, such as pinched or check valves, which may have more limited operational ranges. Thus, the combination of a self-sealing design, efficient flow characteristics, and versatile application makes floating ball valves an optimal choice for industrial piping needs.
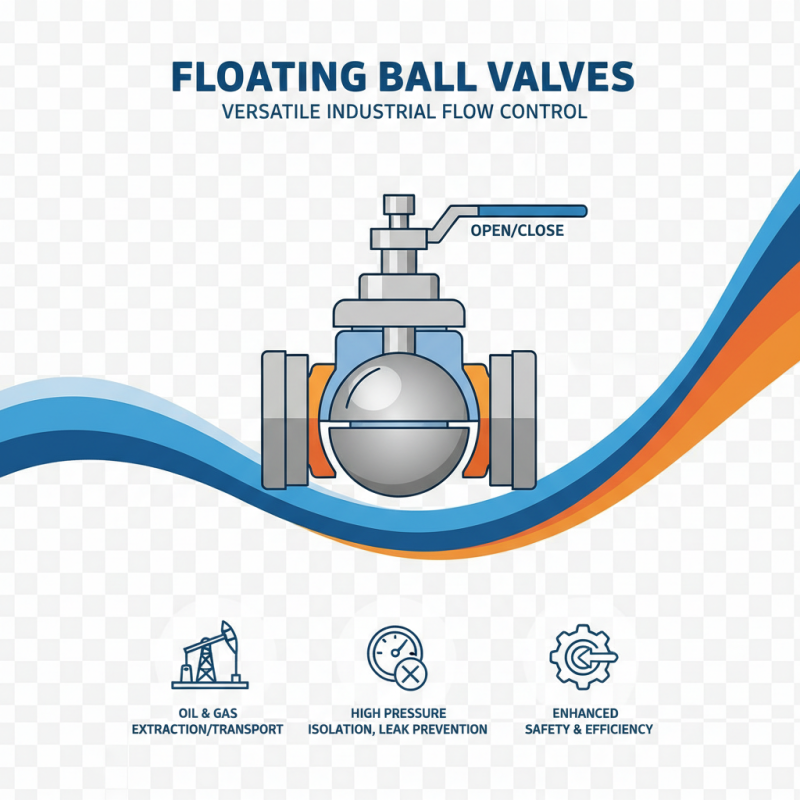
Floating ball valves are versatile components employed across a wide range of industrial applications due to their reliable sealing capabilities and ease of operation. In the oil and gas sector, for instance, these valves play a crucial role in controlling the flow of fluids during extraction and transportation processes. Their design allows for effective isolation even under high pressure, making them ideal for environments where safety is paramount. The smooth operation of floating ball valves minimizes the risk of leaks, thereby enhancing operational safety and efficiency.
In chemical processing, floating ball valves are equally vital. They are commonly used for regulating the flow of corrosive substances, thanks to their resilient construction. These valves operate efficiently in a variety of temperatures and pressures, making them suitable for processes that require precision flow control. Additionally, in water treatment facilities, floating ball valves manage the distribution of treated water while maintaining system integrity. Their ability to withstand harsh conditions and maintain a tight seal makes them indispensable in maintaining quality and safety standards across various industrial sectors.
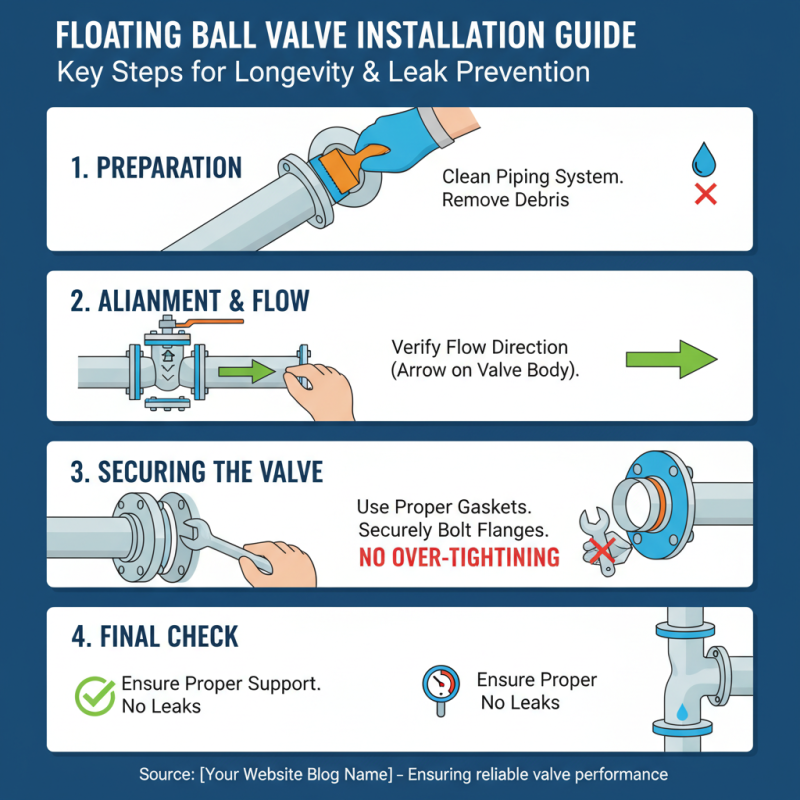
When installing a floating ball valve, it is essential to ensure proper alignment and support. Begin the installation by verifying that the piping system is clean and free of debris. This helps prevent contamination and ensures the longevity of the valve. Position the valve so that the flow direction matches the markings on the body, typically indicated by an arrow. It is crucial to use appropriate gaskets and ensure that the valve is securely bolted to the flanges without over-tightening, which can warp the valve body and lead to leaks.
Maintenance of floating ball valves is relatively straightforward, but routine checks are essential for optimal performance. Regularly inspect the valve for signs of wear, corrosion, or leaks. Lubrication of the stem and other moving parts is necessary to maintain smooth operation and prevent seizing. Additionally, it’s wise to test the valve periodically by operating it through its full range of motion to ensure it opens and closes without obstruction. By adhering to these installation and maintenance guidelines, floating ball valves can provide reliable performance in various industrial applications.
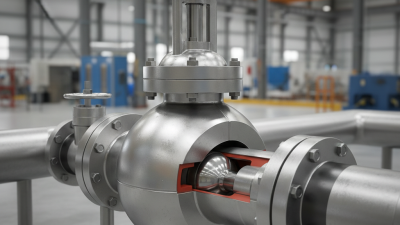
Floating ball valves are increasingly favored in industrial applications due to their unique working mechanism. The design features a ball that is floating, meaning it rests on a soft seat, allowing it to move slightly to ensure a proper seal when the valve is closed. This movement helps accommodate potential misalignments in the piping system, enhancing the valve's reliability and strength against pressure differentials. When the valve is open, the ball allows unrestricted flow, minimizing turbulence and pressure drop within the pipe.
When opting for a floating ball valve, consider the following tips: First, ensure that the valve's material compatibility matches the fluid being transported, as this can prevent corrosion or degradation. Additionally, assess the operating conditions, including pressure and temperature ranges, as these factors greatly influence the valve's performance and lifespan. Finally, regular maintenance checks will help ensure the proper functioning of the valve, avoiding sudden failures that could interrupt operations.
In terms of efficiency, floating ball valves are designed to provide quick on/off control with minimal effort, making them ideal for automated systems. Their simple structure also means that they are easier to install and maintain compared to other valve types. By understanding these fundamental attributes and mechanisms, industries can better leverage floating ball valves to meet their specific piping needs.
When selecting a floating ball valve for industrial applications, ensuring the right size and specifications is critical for efficiency and performance. According to the American National Standards Institute (ANSI), proper sizing helps to minimize pressure drops and flow disturbances, which are crucial for maintaining the integrity of fluid transport systems. A well-sized valve can significantly impact overall system performance; data from the Valves and Actuators Market Reports indicates that improperly sized valves can lead to efficiency losses upwards of 20%, emphasizing the need for careful selection based on accurate flow conditions and pressure requirements.
Moreover, the specifications you choose should align with the media type, temperature ranges, and pressure ratings expected in your system. For instance, the Chemical Engineering magazine reported that different materials used in ball valves can significantly affect their durability and functionality, particularly in corrosive environments.
When evaluating the specifications, it's essential to reference industry standards such as the ISO 5211, which provides guidelines on actuator compatibility, further ensuring that the floating ball valve integrates seamlessly into your piping setup. In summary, meticulous attention to sizing and specifications not only enhances system performance but also prolongs the lifespan of your equipment within industrial applications.
Floating ball valves are essential components in many industrial applications due to their reliable sealing capabilities and ease of operation. However, like any mechanical system, they can encounter common issues that require troubleshooting. One frequent problem with floating ball valves is leakage, often caused by worn-out seals or debris trapped in the valve seat. According to a report by the Valve Manufacturers Association, approximately 30% of valve failures in industrial settings are attributed to seal degradation. Regular maintenance and inspection are critical to identify these wear issues early and ensure optimal valve performance.
Another common issue is the failure to open or close the valve properly. This can result from insufficient actuator force or foreign objects obstructing the ball. A study from the Institute of Mechanical Engineers highlights that improper valve operation can lead to significant downtime, accounting for up to 20% of maintenance costs in some facilities. Troubleshooting such issues often involves checking the actuator and ensuring the system is free from obstructions. Employing proper installation techniques and following manufacturer guidelines can greatly reduce these occurrences, safeguarding the efficiency and safety of operations. Regular training for maintenance personnel on these common issues enhances the longevity of floating ball valves in industrial environments.
: Floating ball valves are known for their reliability and efficiency, achieving a low leakage rate of 0.01% of the inlet flow rate, which is crucial for critical applications. They also offer ease of operation and maintenance, allowing quick isolation of flow and reducing downtime by up to 25% compared to other valve types.
The design allows the ball to float within the seat, transmitting pressure directly to the ball. This ensures a tight seal, which is essential in preventing leaks and maintaining system integrity.
Important factors include fluid characteristics, pressure rating, and temperature range. These considerations ensure that the valve performs optimally in the intended application.
Regular inspection and maintenance can prevent undue wear and tear, enhancing the longevity of the valves and ensuring their reliable operation in the system.
Proper sizing minimizes pressure drops and flow disturbances, which are vital for the efficiency and performance of fluid transport systems. Improperly sized valves can lead to efficiency losses of up to 20%.
Specifications should align with the media type, temperature ranges, and pressure ratings expected in the system. This alignment ensures durability and functionality, especially in corrosive environments.
Industry standards such as ISO 5211 provide guidelines on actuator compatibility, which is essential for ensuring that the floating ball valve integrates well into the piping setup.
Investing in high-quality materials for floating ball valves can enhance their performance and safety, particularly in critical applications and harsh environments.
Floating ball valves can significantly improve system performance by providing a reliable seal, reducing leaks, and minimizing downtime, which collectively contribute to cost savings.
The ease of operation allows for quick flow isolation during maintenance or emergencies, which is crucial for maintaining safety and operational continuity in industrial settings.
Floating ball valves are increasingly favored in industrial piping systems due to their distinct advantages, such as reliable sealing and ease of operation. These valves operate by allowing the ball to float and align itself with the seat, ensuring minimal leakage even under varying pressures. When compared to other valve types, floating ball valves offer superior flow characteristics and are suitable for a wide range of applications across various industries, including oil and gas, water treatment, and chemical processing.
Proper installation and maintenance are crucial for the longevity and efficient performance of floating ball valves. Understanding their working mechanism is key to troubleshooting common issues that may arise, helping maintain optimal functionality. Additionally, selecting the right size and specifications for your specific piping needs ensures that these valves perform effectively, making floating ball valves a smart choice for industrial applications.