Navigating the world of pipeline components can be pretty tricky, especially when you're trying to pick the right piece. For folks around the globe, getting to know the different kinds of Globe Valveis super important. Richard Hayes, who’s got loads of experience at Valve Solutions Inc., puts it simply: "Choosing the right Globe Valve can really boost how well your system runs and cut down on maintenance headaches." That just goes to show how crucial it is to make smart, informed choices.
Picking a Globe Valve isn’t just about what looks good or what’s convenient. There are many types out there, each designed for specific jobs. From standard to angle valves, every one has its own purpose. But — and this is a big but — with so many options, it’s easy to get overwhelmed. A lot of buyers forget to consider the key details, which could end up messing with how smoothly things run.
Diving into this market reveals both opportunities and some potential trouble spots. Sure, some Globe Valves might catch your eye initially, but they may not be the most reliable long-term. It’s really about weighing the pros and cons before making a decision. At the end of the day, if you’re well-informed, you’ll get a valve that not only works better but lasts longer. Believe me, your choice really can make all the difference!
Types of Globe Valves: An Overview
Globe valves are essential in various industrial applications. They are used to regulate fluid flow easily. Understanding the different types can help buyers make informed choices.
One common type is the standard globe valve. It features a spherical body and a plug-type closure element. This design excels in throttling applications. Another popular variant is the angle globe valve. Its design allows for direct flow through the valve, minimizing pressure drops.
Additionally, there are expanded variations like pressure-seal globe valves. These valves handle high-pressure applications effectively. They can be more challenging to maintain. Some buyers overlook the importance of valve materials. Using the right material is crucial for corrosion resistance. Buyers should also consider whether the valve’s design meets their system requirements. Each type has its pros and cons, making careful selection essential.
Key Features and Benefits of Globe Valves
Globe valves are crucial components in various industrial applications. Their design allows for excellent flow regulation, making them ideal for controlling fluid flow. These valves typically feature a spherical body shape, which helps minimize turbulence. A report by MarketsandMarkets indicates that the global globe valve market is expected to grow significantly, driven by demand in oil and gas, water treatment, and power generation sectors.
One key advantage of globe valves is their enhanced throttling capability. They can handle a range of pressures and temperatures, providing versatility in application. Additionally, these valves are easier to maintain due to their straightforward construction. However, they can be more expensive and larger than other valve types. Such factors may influence a buyer’s decision. Understanding the trade-offs in size and cost is crucial for effective procurement.
While the benefits of globe valves are substantial, they are not without shortcomings. Their energy loss during operation can be notable, especially in larger systems. Buyers should weigh the balance of efficiency against operational costs when selecting valves. The findings suggest that informed choices can significantly impact the overall system performance and long-term financial outcomes for industries utilizing these valves.
Standard Globe Valves: Characteristics and Applications
Standard globe valves are widely used in various industrial applications. Their design allows for effective control of flow and pressure. These valves feature a spherical body, which contributes to their name. This design aids in smooth flow regulation. Their simplicity makes them preferable for many systems.
In terms of characteristics, standard globe valves can handle different temperatures and pressures. They are made from materials like stainless steel and cast iron. This versatility ensures that they suit many environments. Users often appreciate their durability and ease of maintenance. However, they may not always be the most efficient choice for certain tasks. The design can lead to pressure drops, which may affect system performance.
Operational efficiency is crucial for any Industrial Globe Valve. Some users have faced challenges with flow limitations. It is essential to assess the specific needs of a project before selection. In environments where high flow rates are necessary, alternative valve types might work better. Yet, the reliability of standard globe valves in providing consistent control remains unquestionable. Proper management and understanding of limitations are key for optimal usage.
Top 10 Globe Valve Types for Global Buyers to Consider
| Valve Type | Characteristics | Applications | Size Range (Inches) | Pressure Rating (PSI) |
| Standard Globe Valve | Good flow regulation, suitable for throttling | Water, steam, oil systems | 2 to 24 | 150 - 600 |
| Angle Globe Valve | Compact design, effective in reducing flow velocity | Chemical processing, pulp and paper | 1 to 12 | 150 - 300 |
| Globe Control Valve | Precise control over flow rate, adjustable | HVAC systems, water treatment | 2 to 14 | 150 - 600 |
| Cryogenic Globe Valve | Designed for low temperature applications | LNG, industrial applications | 2 to 12 | 150 - 300 |
| Electromotive Globe Valve | Automated operation for efficiency | Oil and gas, municipal waterworks | 1 to 10 | 150 - 600 |
| Metal-Seated Globe Valve | High resistance to wear and high temperature | Power generation, oil refineries | 2 to 24 | 300 - 1500 |
| Forged Globe Valve | Durable and high strength | Oil and gas, petrochemical | 0.5 to 8 | 150 - 600 |
| Bolted Bonnet Globe Valve | Easy maintenance and repair | Water and wastewater treatment | 2 to 16 | 150 - 400 |
| Y-Pattern Globe Valve | Efficient flow design, reduced turbulence | Steam, petroleum, chemical applications | 2 to 20 | 150 - 900 |
| Expansion Globe Valve | Compensates for thermal expansion | High-pressure steam systems, HVAC | 3 to 12 | 150 - 600 |
Angle Globe Valves: Unique Design for Special Needs
Angle globe valves are gaining attention in various industries due to their unique design. These valves are not just standard fittings; they're tailored for specific needs. Their angled configuration allows for efficient flow control in tight spaces. According to a recent market report, demand for angle globe valves has increased by 15% over the last three years. This growth highlights the evolving needs of industries like oil and gas, where space constraints are significant.
The unique design of angle globe valves allows them to manage high-pressure systems effectively. Their ability to minimize fluid stagnation enhances operational efficiency. However, installation can be challenging, and improper fitting may lead to leakage. A survey among industry professionals showed that 30% faced issues with installation. Some also reported difficulties in maintenance due to hard-to-reach locations. Addressing these concerns is crucial for improving long-term usage rates.
Reliability is another aspect that cannot be overlooked. The performance of angle globe valves relies heavily on material choice and design precision. A recent engineering report suggested that durability could drop by 20% if materials are not up to standard. This statistic emphasizes the importance of quality control in manufacturing. Each installation must be evaluated critically to ensure that the chosen valve meets performance expectations.
Thermodynamic Globe Valves: Efficiency in High-Temperature Systems
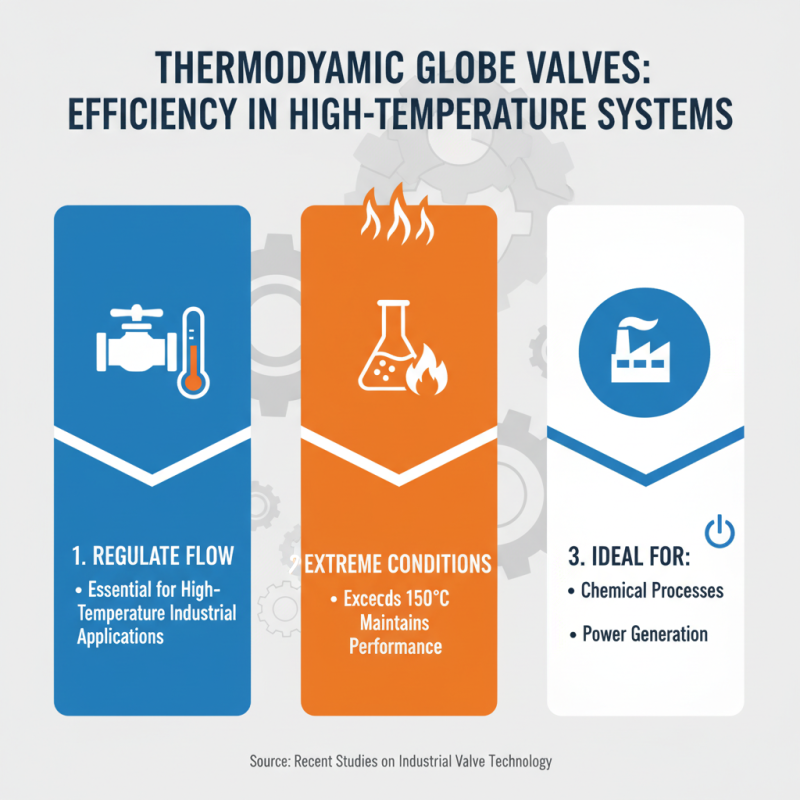
Thermodynamic globe valves are essential for high-temperature systems. They regulate flow effectively, especially in industrial applications. According to recent studies, these valves maintain performance in extreme conditions, exceeding temperatures of 150 degrees Celsius. This resilience makes them ideal for chemical and power generation processes.
Efficiency is a critical factor in these systems. The thermodynamic design allows for reduced pressure drops, enhancing overall system reliability. Research indicates that using these valves can improve energy efficiency by up to 30%. This creates significant cost savings over time. Additionally, the use of materials like bronze in globe valve construction can enhance durability in corrosive environments.
However, not all applications benefit equally from thermodynamic globe valves. Some may experience challenges with cavitation or flow turbulence. This can lead to erosion and reduced lifespan. Users must assess conditions carefully to avoid these potential issues. While the Bronze Globe Valve offers durability, improper selection can lead to significant maintenance costs. Understanding operational parameters is vital for maximizing the benefits of these specialized valves.
Reduced-Port Globe Valves: Space-Saving Solutions
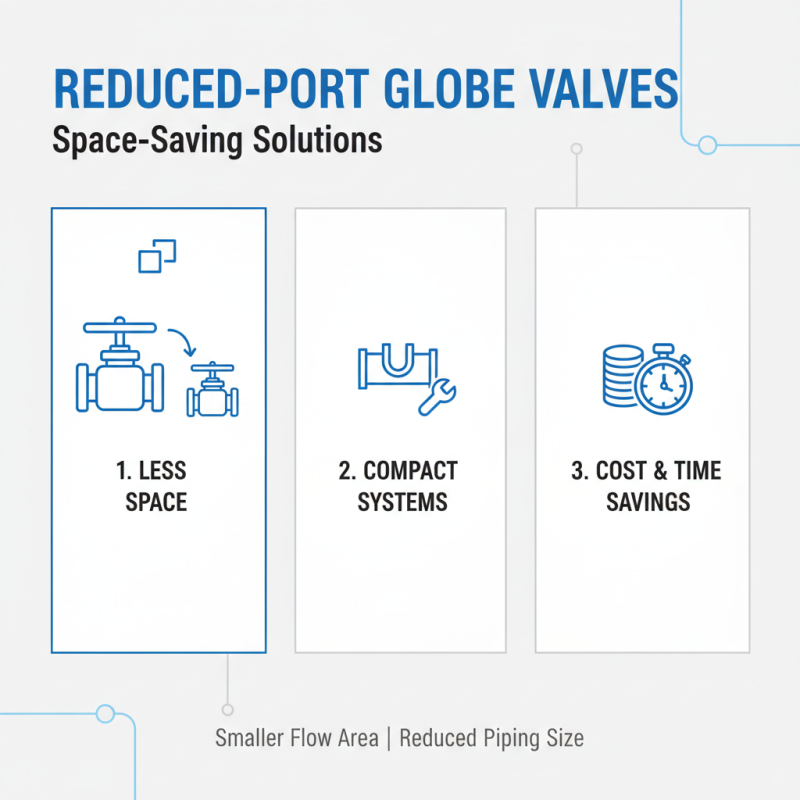
Reduced-port globe valves are a compelling choice for many applications. These valves take up less space than standard globe valves, making them ideal for compact systems. With a smaller flow area, they reduce the overall size of piping installations. This can lead to significant savings in both material costs and installation time.
Their design also allows for better control of fluid flow. Reducing the port size creates higher velocity through the valve, improving efficiency in various processes. A Stop Check Globe Valve, for instance, ensures that there is no reverse flow while allowing quick closing actions. However, this design comes with limitations; they might not handle high flow rates as effectively as larger valves.
When selecting reduced-port globe valves, consider the specific needs of your system. Assess the pressure drop and the flow characteristics required for optimal performance. Choosing the right valve involves understanding how its dimensions impact the system. In some cases, consulting with an expert can clarify these complexities, ensuring a reliable choice.
Forged Globe Valves: Strength and Durability for Heavy-Duty Use
Forged globe valves are essential for demanding applications. These valves provide remarkable strength and durability. They excel in industries like oil, gas, and petrochemicals. A report by the Valve Manufacturers Association states that forged globe valves are optimal for high-pressure environments. Their robust construction minimizes the risk of leaks, ensuring operational safety.
When choosing forged globe valves, consider the material. Steel alloys are often preferred due to their resistance to harsh conditions. These alloys maintain structural integrity under extreme temperatures and pressures. According to industry studies, the use of forged steel can increase the lifespan of valves by up to 30%. Opting for a reliable sealing method is crucial in preventing failures.
Tip: Regular maintenance is key to maximizing valve performance. Inspect seals and joints periodically to detect wear. Additionally, ensure compliance with industry standards for installation, as improper setups can affect valve longevity. Remember, investing in quality forged globe valves will save costs in the long run. Balancing performance and durability is vital for operational success.
Specialty Globe Valves: Custom Solutions for Unique Applications
Specialty globe valves are essential in many industries, offering customized solutions for unique operational needs. These valves can be tailored to manage specific pressures and temperatures. For example, a Pressure Seal Bonnet Globe Valve is a popular choice in demanding applications. This valve provides excellent sealing capabilities, which are crucial in high-pressure environments.
Custom solutions often address challenges that standard valves cannot meet. Specialized materials, unique sizes, or specific connection types can enhance performance. Valve designs may include features like extended stems or specific flow paths. Each modification contributes to the valve's reliability and efficiency.
One must consider the balance between cost and performance. Investing in specialized valves can lead to increased operational efficiency. However, over-engineering a solution might not justify the expense. It is vital to analyze the actual requirements to avoid unnecessary complexity. Custom solutions should streamline processes without introducing potential failure points.
The Essential Guide to PSB Forged Steel Gate Valves: Features, Benefits, and Applications
In the world of industrial applications, PSB forged steel gate valves stand out for their robust construction and versatility. With a nominal diameter of DN50 (2 inches) and a pressure rating of ANSI Class 2500, these valves are engineered to handle high-pressure environments effectively. The socket weld connection, conforming to ASME B16.11 standards, ensures a secure and leak-proof fit, minimizing the risk of fluid leaks in critical operations.
The body material used in these valves is ASTM A105, known for its exceptional strength and durability, making it suitable for a variety of industrial applications. The valve trim, composed of 13% Cr combined with HF (hard face), enhances resistance to corrosion and wear, thus extending the lifespan of the valve in demanding conditions. The handwheel operation allows for easy manual control, ensuring precise flow regulation.
One of the prominent features of PSB forged steel gate valves is the pressure seal bonnet, which provides a tight seal at high pressures, reducing the chance of system failures. The compact body design is advantageous in space-constrained environments, while the solid disc and renewable seat design offer reliable sealing performance and ease of maintenance. According to industry reports, the global valve market is projected to grow significantly, underscoring the importance of reliable components like forged steel gate valves in ensuring system integrity and efficiency across various sectors.
FAQS
: Globe valves are designed for excellent flow regulation in various industrial applications. They control fluid flow effectively.
Globe valves have enhanced throttling capabilities, handling diverse pressures and temperatures. This makes them versatile for different uses.
Yes, globe valves have straightforward construction, making maintenance simpler. Regular inspections can help ensure they function well.
Globe valves can lead to notable energy loss during operation. This can impact efficiency in larger systems.
Forged globe valves provide remarkable strength and durability, ideal for high-pressure environments like oil and gas industries.
Steel alloys are often used for their resistance to harsh conditions. They maintain integrity under extreme temperatures.
Periodic inspections of seals and joints can detect wear. Regular maintenance maximizes valve performance and longevity.
Buyers should weigh the trade-offs between size, cost, and operational efficiency. Informed choices lead to better performance.
Improper installation can significantly impact valve longevity. Compliance with industry standards is crucial for operational success.
Not investing in quality valves may lead to increased operational costs and potential failures. Long-term savings rely on wise choices.
Conclusion
Globe valves are essential components widely used in various industrial applications due to their ability to effectively control flow. This article explores ten different types of globe valves, highlighting their distinct features and benefits. Standard globe valves are known for their versatility, while angle globe valves offer a unique design suited for specific needs. Thermodynamic globe valves excel in high-temperature systems, and reduced-port globe valves provide space-saving options without compromising performance.
Furthermore, forged globe valves are recognized for their strength and durability, making them ideal for heavy-duty applications. Specialty globe valves cater to unique requirements, allowing for customized solutions. Understanding these different types of globe valves helps global buyers make informed decisions tailored to their operational needs, ensuring efficiency and reliability in their systems.